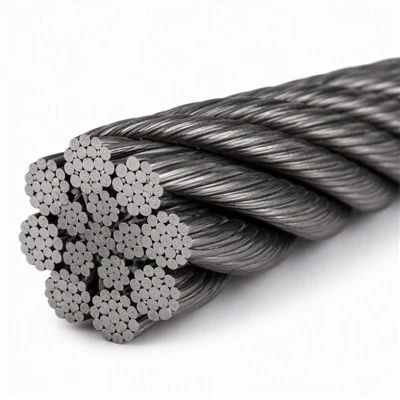
High-Strength Steel Wire Rope for Elevator Safety & Critical Lift Applications
The Heavy Duty Elevator Safety Cable is a premium steel wire rope engineered for safety-critical elevator systems where maximum reliability, strength, and durability are essential. Manufactured from high-quality high-carbon steel with precision stranding technology, this cable provides outstanding tensile strength, excellent fatigue resistance, low elongation, and superior wear performance for long-term operation in demanding environments.
Designed for passenger elevators, freight elevators, industrial lifts, and elevator safety systems, the rope delivers dependable performance under continuous service while meeting the stringent requirements of modern vertical transportation equipment.
Product Features
Engineered for Safety-Critical Applications
Designed for components where reliability is paramount, the cable offers:
High structural stability
Consistent dimensional accuracy
Reliable performance under continuous operation
Long service life
Enhanced operational safety
High Tensile Strength
Manufactured from premium high-carbon steel with nominal tensile grades of:
1570 MPa
1770 MPa
1960 MPa
providing high breaking strength and dependable performance.
Superior Fatigue Resistance
Optimized strand construction minimizes internal wire movement, enabling the rope to withstand millions of bending cycles while maintaining structural integrity.
Excellent Wear & Crush Resistance
Available with Independent Wire Rope Core (IWRC) for applications requiring:
Higher breaking strength
Greater crush resistance
Improved dimensional stability
Reduced structural elongation
Smooth Operation
Precision manufacturing ensures:
Uniform rope diameter
Excellent roundness
Reduced vibration
Stable running performance
Lower traction sheave wear
Corrosion Protection Options
Available with:
Bright (Ungalvanized)
Electro Galvanized
Customized lubrication systems are available to reduce internal friction and improve corrosion protection.
Technical Specifications
|
Item |
Specification |
|
Product Name |
Heavy Duty Elevator Safety Cable |
|
Typical Construction |
6×19S, 8×19S, 8×19W, 8×25Fi, Customized |
|
Material |
High Carbon Steel |
|
Core |
FC / SFC / IWRC |
|
Tensile Strength |
1570 / 1770 / 1960 MPa |
|
Surface Finish |
Bright / Electro Galvanized |
|
Diameter Range |
6 mm – 22 mm (Custom Sizes Available) |
|
Lay Direction |
Right Regular Lay / Left Regular Lay |
|
Lubrication |
Standard or Customized |
|
Manufacturing Standards |
EN 12385, ISO 4344, GB/T 8903, ASTM A1023 (Optional) |
Typical Applications
The Heavy Duty Elevator Safety Cable is suitable for a wide range of elevator safety and lifting applications, including:
- Passenger Elevators
- Freight Elevators
- High-Rise Elevators
- Industrial Elevators
- Service Elevators
- Elevator Overspeed Governor Systems
- Elevator Traction Systems
- Counterweight Systems
- Elevator Hoisting Equipment
- Heavy-Duty Lift Systems
- Maintenance & Modernization Projects
Ideal for applications requiring high load capacity, continuous-duty performance, and maximum operational reliability.

Product Advantages
High tensile strength for demanding applications
Excellent fatigue and wear resistance
Superior dimensional stability
Low elongation for consistent performance
Smooth and quiet operation
Corrosion-resistant finish options
Multiple constructions and core configurations available
Long service life with reduced maintenance
OEM & ODM customization supported
Why Choose Us?
Quality Assurance
Every safety cable is manufactured under a strict quality management system and undergoes comprehensive quality inspections before shipment.
Available documentation includes:
- EN 10204 Type 3.1 Mill Test Certificate
- Material Certificate
- Tensile Test Report
- Breaking Load Test Report
- Diameter & Ovality Inspection Report
- Surface Quality Inspection Report
- Factory Inspection Report
- Packing List
Third-party inspection services by SGS, TÜV, Bureau Veritas (BV), or Intertek are available upon request.


Packaging
Standard export packaging options include:
- Wooden Reel
- Plywood Reel
- Plastic Reel
- Steel Reel
- Moisture-Proof Wrapping
- Customized Export Packaging
Each reel is securely packaged to ensure safe transportation and long-term storage.
Why Choose Solite?
- Professional manufacturer with over 15 years of expertise in steel wire rope production
- Specialized solutions for elevator, lifting, and industrial applications
- Advanced production equipment and precision quality testing
- Strict quality control from raw materials to finished products
- Factory-direct pricing with stable production capacity
- Fast delivery and global export support
- OEM & ODM manufacturing services
- Professional technical assistance for elevator manufacturers, distributors, and maintenance companies